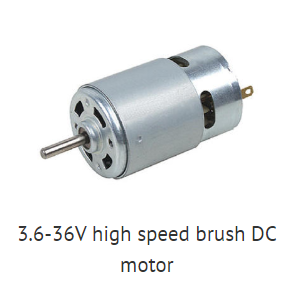
3.6-36V high speed brush DC motor
Applications:
Power tools, air pump, Vacuum Cleaner, Tubular Motor, Automatic Coffee Machine, Charging Fan
Rated Volatge: 3.6-36V
Rated Speed: 2000-24000RPM
Rated Power: 4-145W
Stall Torque: 0.1-0.4Nm
Type: Brush DC motor
Original: Made in China
SMI R-Series weight distribution hitch with sway control system
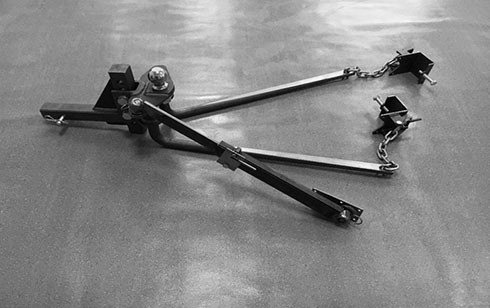
SMI R-Series weight distribution hitch with sway control system
Features:
• Evenly distributes tongue weight to the axles of tow vehicle and trailer for stability and control
– Creates a more level ride for both tow vehicle and trailer
• Friction sway control reduces sway caused by winds, curving roads and sudden maneuvers
– Adjustable tension lets you create the perfect degree of control and resistance
– Integrated handle engages and disengages the system
– Removable – just release 2 spring locking pins
• Round, forged steel spring bars are tapered for superior flexibility
– Bars flex appropriately over uneven terrain for a controlled, even ride
• Adjustable spring-bar tension – just switch links in lift chains to fine-tune
• Desired tilt of head and system is achieved by adding washers to a rivet inside the weight-distribution head
• Solid steel shank is powder coated for rust protection
Specs:
• Tongue weight: 700 lbs to 1,000 lbs
• Gross towing weight: 10,000 lbs
• Fits: 2″ x 2″ trailer hitch receivers rated for use with a weight distribution system
• Shank length: 12-1/2″
• Maximum rise: 6″ from top of hitch receiver opening
• Maximum drop: 2″ from top of hitch receiver opening
• Hitch ball dimensions:
– Diameter: 2-5/16″
– Shank length: 2-1/2″
– Shank diameter: 1-1/4″
SMI G-Series weight distribution hitch

SMI G-Series weight distribution hitch
Features:
• Evenly distributes weight over axles of tow vehicle and trailer for stability and control
– Creates a level ride for both tow vehicle and trailer
• Integrated 4-Point Sway Control limits side-to-side movement
– Brackets keep spring bars in place for a rigid system that holds trailer in line
– Steel-on-steel friction helps to minimize sway caused by winds, curvy roads or sudden maneuvers
– No lift chains – eliminate unwanted movement
• Unique design makes system compatible with surge-type brake actuators
• Spring bars flex for a controlled, even ride
• No-drill, clamp-on brackets can be adjusted along the trailer frame
– Accommodates frame-mounted items such as gas tanks, toolboxes or generators
• Desired tilt is achieved with traditional washer design
– Add or remove washers from spacer rivet to tilt head up or down
• Dipped steel construction is durable and corrosion resistant
• Snap-up lever eases installation by reducing lifting required by trailer jack
Specs:
• Tongue weight: 700 lbs – 1,000 lbs
• Gross towing weight: 10,000 lbs
• Ball size: 2-5/16″
• Fits: 2″ x 2″ trailer hitch receivers rated for use with weight distribution systems
• Lift-bracket positioning: 27″ – 32″ back from center of coupler
• Maximum trailer frame height: 6″
Manganese Casting for Metal-Scraps Shredder

Sino Machine Industry offers a full line of Metal-Scraps shredders castings for the last 24 years. Parts items includes, but not limited as the following:
Grate, Manganese Hammer, Pin Protector, Side Liner, Ejection Door, Anvil, Caps
Feature of Castings:
1) Design to customer requirement;
2) Accurate recommendation of casting chemistry element based on customer’s drawings and descriptions;
3) Complete line for metal-scraps shredder machine castings;
4) Competitive price;
5) Excellent service after sales.
Sow Moulds and DCU (Dross Compression Unit)
DCU Dross Compression Unit — Aluminum Dross Press in Operation
DCU — Dross Compression Unit for Aluminum Dross Recovery
A DCU (Dross Compression Unit) is an aluminum industry term for what is more commonly referred to as an aluminum dross press — a hydraulic compression system designed to recover free metal from hot aluminum dross at the point of generation. The terminology differs across markets and operations; the engineering objective is the same: compress hot dross rapidly under controlled hydraulic force, arrest oxidation through integrated cooling, and produce a dense aluminum block with the maximum recoverable metal content.
SMI designs, manufactures and supplies DCU systems as part of its complete aluminum dross press equipment range. SMI DCU systems are the product of over 30 years of casthouse operational experience and continuous engineering development — incorporating design improvements that directly address the geometric and thermal limitations of earlier dross compression unit designs in the industry.
Early dross compression unit designs relied on pan geometries that prioritised volume over seal integrity — a trade-off that limited recovery performance under sustained operational pressure. SMI’s DCU development addressed these geometric limitations directly: tighter mating tolerances between press head and dross pan, improved thermal seal design, and material formulations engineered specifically for the thermiting conditions of hot dross service. The result is measurably better metal recovery and longer component service life under continuous casthouse operation.
SMI Dross Compression Unit — In Operation
The following video demonstrates an SMI DCU installation in active casthouse service. This footage shows an early production configuration — current SMI DCU systems incorporate significant design and material improvements over the configuration shown, reflecting ongoing engineering development based on operational feedback from casthouse installations worldwide.
The video illustrates the core DCU operating cycle: dross pan positioning, hydraulic head descent, compression under controlled pressure, forced cooling activation, and head retraction. The automated cycle requires no manual intervention during pressing, reducing operator exposure to radiant heat and fume while eliminating the skill variability associated with manual dross handling.
DCU System Design — Key Engineering Principles
Press Head and Dross Pan — The Matched Set
The performance of any DCU system is determined primarily by the quality of the match between the press head (cooling head) and the dross pan. The two components must be designed together — the press head profile must seat correctly against the dross pan walls to maintain an effective thermal seal under hydraulic pressure and transfer heat efficiently through the cooling circuit. SMI designs and supplies press heads and dross pans as matched sets for this reason.
Proprietary Material Formulation
SMI press heads and dross pans are manufactured from a proprietary material formulation developed in-house — engineered for thermal shock resistance and dimensional stability under repeated high-temperature cycling. This formulation is the same specification used across SMI’s full range of casthouse consumables, with a 30-year operational record in aluminum casthouses across multiple continents.
Compatibility Across All Dross Types
SMI DCU systems are configured and validated for the full range of industrially relevant dross types — dry, wet, black, white, salt and rotary furnace slag. Each dross type behaves differently under compression; SMI application engineers confirm the correct press head geometry, cooling configuration and dross pan specification for each installation’s specific dross characteristics before order placement.
Upgrade and Retrofit
For operations with existing DCU or dross press installations from any manufacturer, SMI provides upgrade and retrofit supply — replacement press heads, dross pan sets and system improvements — without requiring full system replacement. Where the press frame is serviceable, targeted component upgrades can deliver significant improvements in recovery performance. All third-party press frame adaptations are subject to engineering review before supply confirmation.
Sow Moulds — Overview
SMI also supplies alloy steel sow moulds for aluminum casthouses. Sow moulds are reusable cast steel moulds used to form aluminium ingots and cast molten metal from furnaces and transfer launders. SMI sow moulds are manufactured from proprietary alloy steel formulations engineered for thermal shock resistance and long service life in continuous casthouse operation.
Standard and low-profile designs are available in multiple sizes, with options for air-cooled applications, sow feet, lugs and hooks, fork channels, and application-specific material chemistries. Custom configurations — including logo casting and dimensional modifications — are available on request. For the full sow mould product range and specifications, see the SMI Alloy Steel Sow Mould and Dross Skim Pans and Sow Moulds pages.
Related Products — Complete Dross Management from SMI
- Aluminum Dross Press Systems — SMI40, SMI60, SMI80 and custom configurations
- Dross Press Cooling Head — cooled and uncooled variants, all geometries
- Dross Press Equipment Overview — system configurations and upgrade options
- Dross Skim Pans and Sow Moulds — matched pan-and-head sets
- Aluminum Dross Cooling Pan — rapid salt cake cooling post-press
- Aluminum Dross Recycling Systems — full downstream processing line
- Alloy Steel Sow Moulds
- Ingot Molds, Sow Moulds and Dross Pans for Aluminum Scrap Recycling
Request a Quotation or Technical Consultation
To discuss DCU system requirements, press head and dross pan configuration, or sow mould specifications, please contact SMI’s application engineering team with the following information:
- Operation type: primary smelter / secondary smelter / recycling plant
- Furnace type and dross generation rate
- Dross type: dry / wet / black / white / salt / rotary furnace slag
- Existing equipment: press frame, pan set, cooling system if applicable
- Sow mould requirements: standard / low-profile / custom dimensions
SMI Dross Processing in Aluminum Recycling Operations
Dross Processing in Aluminium Recycling Operations — Pan Design, Press Configuration and Why Results Vary
SMI has been supplying dross pans and dross press systems to the aluminium industry for over 30 years. Since 2009, Mr. David Roth has been our head consultant, bringing decades of experience in the global aluminium industry to SMI’s equipment design and customer application work.
All of the major players in aluminium melting and casting have purchased SMI quality castings. The observations in this article are drawn from that operational experience — from installations that worked well and from installations that did not, and from understanding precisely why the difference occurred.
The Dross Pan — Where Recovery Begins
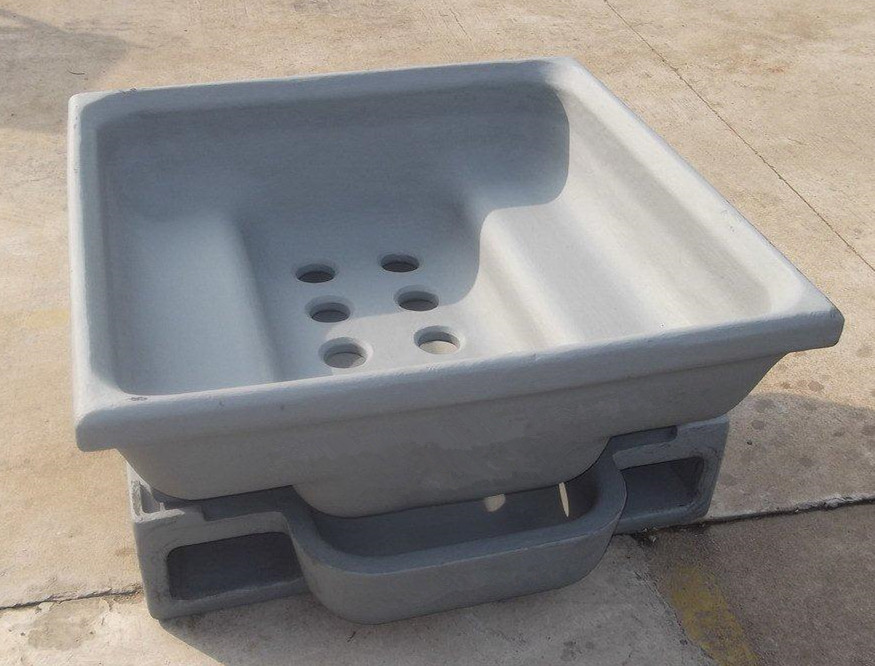
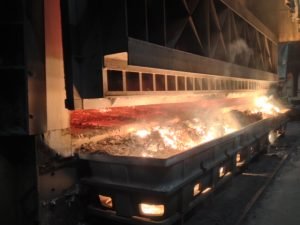
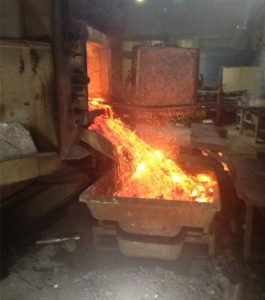
The dross pan is not a passive container. Its design directly determines how much metal is recovered in the pressing cycle that follows. The unique characteristics of SMI’s dross pan design allow for a significant degree of cooling contact between the dross and the cast steel — a function of pan mass, geometry and surface area that cannot be replicated by a simple fabricated vessel.
The drain hole configuration is a specific engineering decision, not a standard feature. The number of holes and the double counter-sink design allows for the maximum drain possible without dross sticking in the holes — a failure mode that renders the drain function ineffective and forces operators to intervene manually. The distance between the skim position and the sow mould is also considered carefully in the pan design, to allow large drain volumes without the pans freezing together during the transfer process.
The cooling cycle for correctly specified dross pans is approximately two hours before the material can be rotated out. The large pan mass is critical to achieving this result — it is what drives the thermal extraction that makes the subsequent pressing cycle effective.
Some earlier pan designs in the industry relied on single-hole drain configurations. A single drain point is inherently prone to blockage given the viscosity and oxide content of hot dross — when it blocks, the entire drain function is lost. The single-chamber pan geometry also limits the cooling and plating action achievable during pressing. SMI’s multi-hole, double counter-sink design addresses both failure modes directly.
Press Capacity — The Operational Variable Most Often Underestimated
The most consistent cause of dross press underperformance in the field is not equipment quality — it is insufficient press capacity relative to the dross generation rate of the operation.
The mechanism is straightforward. Hot dross skimmed from the furnace begins oxidising immediately. The cooling and plating action that is the primary benefit of pressing — the conversion of liquid aluminium droplets into a recoverable solid block — requires the dross to reach the press while still at temperature. If a dross pan sits for more than 15 minutes before pressing, this process is already significantly compromised. The dross has cooled, the liquid aluminium has partially oxidised, and the pressing cycle produces a result that does not reflect the capability of the equipment.
When multiple pans queue in front of a single press, the pans at the back of the queue are already cold before they are processed. Operators observe poor results, conclude that pressing is ineffective, and gradually stop using the equipment — not because the press is at fault, but because the system was never configured with adequate capacity for the volume of dross being generated.
The practical implication for system specification is direct: the number of presses required for an operation is determined by the dross generation rate and the 15-minute processing window — not by capital budget alone. An undercapacity installation does not produce partial results; it produces results that appear to confirm that pressing does not work, which is a different and more damaging outcome.
The Pan and Press Head as a Matched System
The most important engineering decision in a dross press installation is the casting design of the pan and the press head as a matched pair. The press head must seat correctly against the pan walls to maintain an effective seal under hydraulic pressure — a poor geometric match allows dross to escape under compression and breaks the thermal contact that drives cooling performance.
SMI designs the pan and press head together, specifically for each customer’s furnace configuration, dross volumes and material handling capabilities — fork truck specifications, transfer distances and pan positioning. The combination of pan design and press head geometry determines the fastest possible cooling rate, the highest achievable drain volume and the most effective plating action for the specific dross type being processed.
The press itself — hydraulics, frame, automation — is in SMI’s view a delivery mechanism for the casting design. A high-quality press delivering poor results is almost always a pan-and-head geometry problem, not a press problem. SMI’s focus is on providing a high-quality, simple, low-maintenance press that fully utilises the recovery capability built into the casting design.
Operational Recommendations
Based on over 30 years of dross press installations across primary smelters, secondary smelters and recycling operations, SMI’s application engineering team consistently observes the following in operations that achieve the best results:
- Minimise time from skimming to pressing — the 15-minute window is a real operational constraint, not a guideline. Workflow design should prioritise getting hot dross to the press as the first priority after skimming.
- Size press capacity to dross generation rate — calculate the number of pans generated per shift and confirm that press capacity can process them all within the 15-minute window. If the numbers do not support a single press, two presses is the correct specification.
- Specify pan and press head as a matched set — do not select the press and the pan independently. The geometric relationship between them is the primary determinant of recovery performance.
- Maintain the pan-to-head seal — a worn or damaged mating face on either the pan or the head degrades recovery performance continuously. Replacement scheduling should be based on dimensional inspection, not visible failure.
- Account for dross type — different furnace types and alloy practices produce dross with different characteristics. Pan and head geometry should be confirmed for the specific dross type being processed, not selected from a generic catalogue.
SMI Dross Pan Design — Key Features
| Design Feature | Function | Failure Mode Addressed |
|---|---|---|
| Multi-hole drain configuration | Maximum drain volume during pressing | Single-hole blockage — loss of drain function |
| Double counter-sink hole design | Prevents dross sticking in drain holes | Hole blockage requiring manual intervention |
| Large pan mass | Thermal mass drives cooling contact with dross | Insufficient cooling — poor plating action |
| Pan-to-head matched geometry | Effective seal under hydraulic pressure | Dross escape and thermal seal failure under compression |
| Furnace-specific dimensioning | Correct volume for furnace dross output | Undersized or oversized pans relative to dross generation |
| Fork truck compatibility | Safe transfer from furnace to press | Handling delays that extend the pre-press window beyond 15 minutes |
Related Products
- Dross Skim Pans and Sow Moulds — matched pan-and-head sets, proprietary alloy steel
- Dross Press Cooling Head — cooled and uncooled variants, all geometries
- Aluminum Dross Press — SMI40, SMI60, SMI80 and custom configurations
- Dross Press Equipment Overview — system configurations and upgrade options
- Press Head and Dross Pan — matched configuration guide
- Aluminum Dross Cooling Pan — post-press salt cake and dross cooling unit
- Aluminum Dross Recycling Systems — complete downstream processing line
Contact SMI — Dross Processing Application Enquiry
To discuss dross pan and press head specification for your operation, or to review an existing installation that is not achieving expected recovery results, please contact SMI’s application engineering team. Please provide your furnace type, dross generation rate per shift, current pan and press configuration, and dross type.
SMI will respond with a written assessment and recommendation. Contact SMI →