• Skip to main content
  • Skip to primary sidebar
  • Skip to footer

Sino Machine Industries

  • Home
  • About Us
  • Industries Served
    • SMI Products Overview
      • SMI Special Steel Products 01
      • SMI Special Steel Products 02
      • SMI Metal Recycling
      • NDT (Non Destructive Testing) service
  • Capabilities
    • Aluminum Industry
      • Aluminum Dross Press
      • Aluminum Dross Cooling Pan
      • Alloy Steel Sow Mold
      • Aluminum Dross Skim Blades and Skim Tools
      • Aluminum Furnace Skimming Tool or Skim blades used for Stirring and Mixing
      • Dross Press & Dross Processing
      • Application of Intelligent Ladle Slag Scraper (Skimming Tools) in steel mills and aluminum mills
      • Transmission Parts
      • The correct combination of the press head and the dross pan
      • 7-9kgs Small Standard Ingot Molds | Moldes de lingotes estándar pequeños de 7-9kgs
      • Comparison between Sow Molds and Ingot Molds
      • Aluminum Dross Transport Equipment
      • Aluminum Dross Recycling Systems
      • Aluminum, Magnesium, Brass, Bronze, Lead, Zinc Ingot Molds
      • Anode steel claw (Electrolytic claw) | Garra de acero del ánodo (garra electrolítica)
      • Anode Steel Yoke
  • eNews
  • Contact Us
You are here: Home / Archives for Aluminium Industry Equipment / Dross Management

Dross Management

February 16, 2023 By Coffy Leave a Comment

Aluminum Dross Recycling Systems

Aluminum Dross Recycling Systems-1
Aluminum Dross Recycling Systems-2
Aluminum Dross Recycling Systems-3

With unique design, our aluminum dross recycling system manage the hot dross very effectively , the oxidation and metal loss will be terminated in a very short time, in-house metal recovery could be 70-80%, much higher than any other solutions.

The Aluminum Dross Recycling System covers the following equipment.

Dross stirrer
Dross cooler
Crusher and screening machine
Dust collector
Conveyor

Aluminum Dross Recycling Systems (partial photographs)

Filed Under: Dross Management Tagged With: aluminium recycling, Aluminum Dross Recycling Systems, Dross Press, metal recovery, secondary smelter

January 23, 2023 By Sen Liang Leave a Comment

Dross Press Cooling Head

Dross Press Cooling Head — Aluminum Dross Press Component Supply

The dross press cooling head is the component that determines how much aluminum you actually recover from hot dross. Aluminum dross oxidises continuously after leaving the furnace — the cooling head must contact the dross quickly, seal tightly against the pan walls, and extract heat fast enough to arrest that oxidation before free metal is lost irreversibly.

SMI manufactures dross press cooling heads as a standalone supply item and as part of complete aluminum dross press systems. As an aluminum recycling systems integrator with in-house material development, casting manufacture and on-site installation capability, SMI supplies cooling heads not simply as cast components to a drawing — but as engineered parts of a complete dross management solution. Cooled and uncooled variants are available across all geometries and sizes, matched to any dross pan or press frame currently in service.


Cooled and Uncooled Configurations

SMI dross press cooling heads are available in cooled and uncooled configurations. The appropriate variant is determined by the specific operational requirements of each installation — furnace type, dross generation rate, existing cooling infrastructure, press cycle objectives and overall system design. Cooled heads incorporate an integrated forced-cooling circuit and are the standard recommendation where maximising metal recovery and minimising oxidation time are the primary objectives. Uncooled heads are available for installations where the process configuration, existing infrastructure or operational parameters make active cooling in the head unnecessary. Both configurations are manufactured from the same SMI ATM series castable and are available across the full range of geometries. SMI application engineers will confirm the most suitable configuration based on a review of process parameters at the enquiry stage.


How the Cooling Head Determines Your Recovery Rate

The dross press works on a single principle: compress and cool hot dross as quickly as possible after skimming, before oxidation converts free metal into oxide. The cooling head is where that principle either succeeds or fails. Four variables determine performance in practice:

  • Seal geometry — the head profile must match the dross pan walls precisely. A poor fit allows dross to escape under pressure, breaks the thermal seal, and extends cooling time. Recovery loss from a worn or mismatched head is continuous and largely invisible until a direct measurement is taken.
  • Active heat extraction — forced cooling through an integrated circuit in the head body produces the cooling rates needed to arrest oxidation effectively. Passive ambient cooling is not sufficient for high-throughput operations.
  • Thermal shock resistance — the head enters dross at 700°C+ and is then cooled, dozens of times per shift. Material that cracks, spalls or deforms under this cycling degrades both seal geometry and cooling performance simultaneously — progressively and invisibly until failure.
  • Dimensional stability over service life — wear and thermal deformation on the mating face progressively degrade the head-to-pan seal. Material choice and casting geometry determine how long a head remains dimensionally effective before replacement is required.

SMI cooling heads are engineered around all four of these failure modes. The design objective is consistent, measurable performance across the full service life of the head — not only at initial installation.


Design and Manufacturing

Proprietary Anti-Thermal-Shock Castable — SMI ATM Series

The cooling head material is the central engineering decision and the point where most generic or cost-reduced heads fail prematurely. A dross press cooling head requires three material properties simultaneously: high thermal conductivity in the cooling zone to extract heat efficiently; low thermal expansion to resist cracking under repeated thermal shock; and abrasion resistance against the hard aluminum oxide particles present in all dross types. Standard refractory grades are optimised for one or two of these properties — not all three together.

SMI’s ATM series material is developed and produced in-house. The formulation is proprietary. Independent third-party test data and material samples are available to qualified buyers on request. This is the same material specification used across SMI’s full range of casthouse consumables — a production-grade specification with a 30-year operational record in aluminum casthouses across multiple continents.

Cast-In Cooling Circuit

The internal cooling channels in an SMI cooled head are formed during the casting process as part of the original geometry — not machined in afterward. Machined-in channels create walls of non-uniform thickness at the cooling zone, producing stress concentration points that initiate cracking under thermal cycling. Cast-in channels maintain consistent section thickness throughout the head body, producing more uniform heat extraction and longer dimensional stability under service conditions. The cooling circuit interfaces with the press cooling skid via standardised quick-connect fittings, allowing head replacement without draining the cooling loop.

Pan-Matched Geometry

SMI supplies cooling heads in circular, rectangular and custom cross-sections. Where a customer has an existing pan set, SMI manufactures replacement heads to match the pan geometry exactly. Where a complete new pan-and-head set is required, the two are designed together to optimise the seal profile and heat transfer path as a matched system. Dimensional tolerances on mating surfaces are held to ±1 mm. The pan-and-head combination is the single configuration decision with the largest impact on achievable in-house recovery rate — SMI designs and supplies both as a matched set for this reason.

Adaptation to Third-Party Press Installations

SMI cooling heads can be adapted to work with third-party and competitor press installations. This is a relevant supply option for operations with serviceable press frames where heads have worn, cracked or degraded, and full system replacement is not the preferred route.

A dimensional match on the head body and mating face is the starting point, not the complete solution. Hydraulic output, control system parameters, cycle timing and commissioning requirements vary significantly between press manufacturers and models — these are not visible in the physical dimensions of the head alone. SMI conducts a technical review of the existing press system specifications before confirming the adaptation scope and supply terms. This engineering review is SMI’s standard process for delivering a qualified, system-compatible solution.

The full delivery scope for third-party adaptations — engineering review, component manufacture, on-site installation and commissioning — is available as a single-source engagement. Buyers are requested to provide press equipment specifications, hydraulic system data and available press documentation at the enquiry stage.


Dross Type Coverage

Dross composition and behaviour under compression varies significantly by furnace type, alloy, flux practice and holding time. SMI cooling heads are specified and validated for the full range of industrially relevant dross and slag types:

  • Dry dross — primary smelter, low oxide content, high free metal fraction
  • Wet dross — holding furnace, alloying additions, variable metal content
  • Black dross — salt-flux secondary smelting, elevated chloride content
  • White dross — secondary smelter pre-treated, lower free metal content
  • Salt slag — rotary furnace with salt flux, requires specific head geometry and cooling duty
  • Rotary furnace slag — high temperature, lower aluminum content, variable composition

For dross with unusual characteristics — very high free metal, atypical particle size distribution, elevated impurity content — SMI application engineers review the process parameters and recommend the correct head geometry, cooling configuration and material grade before order placement.


Operational Benefits

Measurable Improvement in In-House Metal Recovery

Faster cooling means less oxidation between pressing cycles. Tighter compaction means fewer voids where trapped metal remains inaccessible. In-house recovery with a correctly configured pan-and-head system typically reaches 45–70%, substantially above unpressed or air-cooled dross handling. One practical constraint: if a dross pan sits for more than 15 minutes with hot dross before reaching the press, thermiting has already progressed significantly. Adequate press capacity relative to dross generation rate is a prerequisite — the cooling head design cannot compensate for insufficient press throughput.

Automated Cycle — Reduced Operator Exposure

The dross press cycle is fully programmable and automated: the head descends, holds at set pressure, cooling is confirmed, and the head retracts. No manual intervention is required during pressing. This removes operator exposure to radiant heat and fume, eliminates skill variability in dross handling, and reduces the specialist knowledge required for day-to-day operation and maintenance.

Schedulable Consumable Cost

Replacement heads are a known, foreseeable consumable cost — not an unplanned capital event. SMI ATM series material and robust casting process support extended and predictable service life under sustained thermal cycling. Replacement heads for common press formats are held in stock; non-standard and legacy press frame heads are manufactured on short lead times. Quality documentation — dimensional inspection reports, material certification, hardness test data — is supplied as standard with every order.


Specifications at a Glance

Parameter Details
Material SMI ATM series — proprietary anti-thermal-shock castable, 30+ year production record
Configurations Cooled (integrated forced-cooling circuit) and uncooled — both available in all geometries, confirmed by application review
Cooling system (cooled variant) Cast-in internal circuit; forced cooling; quick-connect interface to press cooling skid
Available geometries Circular, rectangular, custom cross-section — new design or matched to existing pan
Press frame compatibility SMI press systems; third-party and competitor frames subject to engineering review and system specification confirmation
Dross types covered Dry, wet, black, white, salt slag, rotary furnace slag
Mating face tolerance ±1 mm on pan-matched sealing surfaces
Typical in-house recovery 45–70% with matched pan-and-head set, correctly configured
Quality documentation Dimensional inspection, material certification, hardness test data — standard with every order
Delivery scope Component supply only; matched pan-and-head set; or complete system including engineering review, installation and commissioning

Global Casthouse Supply — Who Uses SMI

SMI has been supplying aluminum recycling systems and casthouse consumables since 1996, with over 30 years of manufacturing and export experience across legal entities in mainland China, Hong Kong, Southeast Asia, Europe and the United States.

SMI casthouse consumables — including dross press cooling heads, dross pans, sow molds, drain sow molds and ingot molds — are in active service at primary aluminum smelters across the Middle East, Europe, India, North America and Asia-Pacific, including multiple operations within the world’s highest-output primary aluminum production groups. Global adoption of SMI dross pans, sow molds and ingot molds continues to accelerate as smelters and recycling operations standardise on SMI as their casthouse consumable supplier of choice.

All supply relationships are subject to confidentiality agreements. Reference accounts are available to qualified buyers under appropriate confidentiality terms.


Application Sectors

  • Primary aluminum smelters
  • Secondary aluminum smelters and refineries
  • Aluminum rod, billet and bar plants
  • Metal recycling and non-ferrous scrap processing plants
  • Aluminum die casting and foundry operations
  • Magnesium and other non-ferrous metal recovery operations

Related Products — Complete Dross Management from SMI

  • Aluminum Dross Press — complete press systems for primary and secondary aluminum operations
  • Dross Press Equipment Overview — system configurations, capacity planning and upgrade options
  • Dross Skim Pans and Sow Molds — pan-and-head matched sets for maximum in-house recovery
  • Aluminum Dross Cooling Pan — rapid salt cake cooling post-press
  • Dross Skim Blades and Casthouse Skimming Tools
  • Aluminum Dross Recycling Systems — full downstream processing: stirrer, cooler, crusher, screening and dust collection
  • Alloy Steel Sow Molds
  • Alloy Steel Ingot Molds, Sow Molds and Dross Pans for Aluminum Scrap Recycling

Request a Quotation or Technical Consultation

To specify the correct cooling head configuration for your operation, please provide the following when contacting SMI:

  • Press frame make, model and existing head dimensions (drawing, dimensional sketch or physical sample)
  • Dross pan design — drawing reference or internal dimensions
  • Dross type and approximate monthly dross volume (tonnes per month)
  • Operation type: primary smelter / secondary smelter / recycling plant
  • For third-party press installations: hydraulic system specifications and available press documentation

SMI will respond with a written technical recommendation and commercial proposal. Contact SMI — Dross Press Cooling Head Enquiry →

Filed Under: Dross Management Tagged With: aluminium dross, cooling head, Dross Press, dross press parts, press head replacement

April 10, 2022 By Sen Liang Leave a Comment

Aluminium Dross Recycling Machine

Aluminium Dross Recycling Machine — Dross Press Systems for Aluminium Casthouses

An aluminium dross recycling machine is the operational term used across many aluminium casthouses for what engineers specify as an aluminium dross press — a hydraulic compression system that recovers free metal from hot aluminium dross at the point of generation, before oxidation converts recoverable aluminium into oxide waste.

SMI has been manufacturing and supplying aluminium dross recycling machines to primary smelters, secondary smelters and metal recycling operations worldwide for over 30 years. Equipment is supplied under the SMI brand, under OEM arrangements, or under the customer’s preferred brand identity — configuration, capacity and branding are all subject to customer specification. The image below shows one such installation, supplied to customer specification.

SMI Aluminium Dross Recycling Machine
Aluminium Dross Recycling Machine — hydraulic dross press with integrated cooling system, supplied to customer specification.

What the Machine Does — The Operational Reality

Hot aluminium dross skimmed from the furnace is not waste. It contains significant free metal — the exact proportion depends on furnace type, alloy, operating practice and how quickly the dross reaches the press after skimming. Every minute of delay between skimming and pressing allows continued oxidation, converting recoverable aluminium into aluminium oxide at a rate that represents a direct production loss on every cast.

The dross recycling machine addresses this at the source. The automated press cycle — hydraulic head descent, compression at controlled pressure, forced cooling through the integrated cooling circuit, head retraction — processes a full pan of hot dross in a single cycle. No manual intervention is required during pressing. The output is a dense aluminium block with significantly reduced oxide content, ready for return to the furnace or casting line.

In-house metal recovery with a correctly configured dross press system is typically 20–35%, depending on operational conditions. The variables that most affect recovery rate in practice are the time elapsed between skimming and pressing, the condition of the press head and dross pan as a matched set, and the dross generation characteristics of the specific furnace operation.


How SMI Supplies Dross Recycling Machines

Standard SMI-Branded Systems

SMI supplies aluminium dross press systems under the SMI brand in three standard capacity configurations — SMI40, SMI60 and SMI80 — processing 250–700 kg of dross per pressing cycle. Full technical specifications, hydraulic component details and delivery terms are covered on the Aluminum Dross Press product page.

OEM Supply

SMI manufactures dross press systems for supply under OEM arrangements — where the equipment is integrated into a customer’s own product line, system package or project supply. OEM customers receive the same manufacturing quality and engineering support as direct SMI-branded supply, with configuration, capacity, labelling and documentation adapted to the OEM customer’s requirements. NDA-based supply is standard practice for OEM engagements.

Custom-Branded and Customer-Specified Equipment

Where a customer operates under their own equipment brand, or has specific requirements for branding, colour, control system interface or documentation language, SMI accommodates these requirements as part of the supply specification. Custom-branded dross press systems have been supplied to aluminium operations across multiple regions — the equipment in service carries the customer’s identity; the engineering and manufacturing capability behind it is SMI’s.

Configured to Your Operation

No two casthouse installations are identical. SMI dross recycling machine configurations take into account the full operational context of each installation — furnace type and capacity, dross generation rate, material handling constraints, available utilities and the dross characteristics specific to each operation. The press head and dross pan combination is specified as a matched set for each installation, as this pairing has the largest single impact on achievable recovery rate.


Dross Press as Part of a Complete Recovery Line

The dross press is the first and most critical stage in aluminium dross recovery — but it is not the only stage. Pressed dross still contains residual metal in the form of fine aluminium particles within the oxide matrix. A complete recovery line processes this residual material through controlled cooling, ball mill crushing and multi-stage vibrating screen separation, producing three separated fractions: metal-rich particles returned to the furnace, intermediate material recycled through the press, and fine aluminium oxide powder for industrial resale.

SMI supplies the complete downstream processing line as well as the dross press stage. For operations building out their dross recovery capability in stages, individual equipment items — cooling unit, ball mill, screening system — can be added progressively. Details of the downstream processing equipment are covered on the Aluminum Dross Recycling Systems page.


Upgrade and Replacement Supply

For operations with existing dross press installations — whether SMI-supplied or from other manufacturers — SMI provides replacement and upgrade supply across the consumable and component range. The press head (cooling head) and dross pan set are the components that most directly determine ongoing recovery performance and are the most common upgrade focus in existing installations.

Where the press frame is serviceable but recovery performance has declined, targeted component replacement typically delivers a measurable improvement without the capital requirement of full system replacement. Third-party press frame adaptations are subject to engineering review before supply confirmation — hydraulic output, control parameters and commissioning requirements vary between press manufacturers and must be confirmed before a compatible replacement head can be specified.


Application Sectors

  • Primary aluminium smelters
  • Secondary aluminium smelters and refineries
  • Aluminium rod, billet and bar plants
  • Metal recycling and non-ferrous scrap processing plants
  • Aluminium die casting and foundry operations
  • OEM equipment integrators and aluminium plant system suppliers

Global Supply and Service

SMI has been supplying aluminium dross recycling machines and casthouse consumables since 1996, with over 30 years of manufacturing and export experience across legal entities in mainland China, Hong Kong, Southeast Asia, Europe and the United States. SMI dross press equipment is in active service at primary and secondary aluminium smelters across the Middle East, Europe, India, North America and Asia-Pacific, including multiple operations within the world’s highest-output primary aluminium production groups.

Equipment is supplied as complete systems with on-site installation and commissioning support. Replacement consumables — press heads, dross pan sets — are held in stock for common configurations and dispatched on short lead times. All supply relationships are subject to confidentiality agreements. Reference accounts are available to qualified buyers under appropriate confidentiality terms.


Related Products — Complete Dross Management from SMI

  • Aluminum Dross Press — SMI40, SMI60, SMI80 specifications and delivery details
  • Dross Press Cooling Head — cooled and uncooled variants, all geometries
  • Dross Press Equipment Overview — system configurations and upgrade options
  • Dross Skim Pans and Sow Moulds — matched pan-and-head sets
  • Aluminum Dross Cooling Pan — post-press salt cake and dross cooling unit
  • DCU Dross Compression Unit — dross press in operation, video
  • Aluminum Dross Recycling Systems — complete downstream processing line
  • Alloy Steel Sow Moulds

Request a Quotation or Technical Consultation

To discuss dross recycling machine requirements — standard SMI-branded systems, OEM supply, or custom-configured equipment — please contact SMI with the following information:

  • Operation type: primary smelter / secondary smelter / recycling plant / OEM integrator
  • Furnace type and approximate dross generation rate per shift
  • Dross type: dry / wet / black / white / salt / rotary furnace
  • Supply requirement: complete system / replacement components / OEM arrangement
  • Branding and documentation requirements if applicable

SMI will respond with a written technical recommendation and commercial proposal. Contact SMI — Aluminium Dross Recycling Machine Enquiry →

Filed Under: Dross Management Tagged With: aluminium dross, aluminium recycling, dross processing equipment, dross recycling, metal recovery

March 29, 2021 By Sen Liang Leave a Comment

Large Cooling Pan

Large cooling pan:
For steel casting, rolling, heat treatment, quenching, and other metallurgical processes.
Premium high-strength steel, stiffness and wear resistance.
The cooling speed is fast, and the cooling effect is uniform, and it is not easy to produce defects such as cracks and deformation.
Can be customized meet needs, product quality is stable.

Product Description:
Our high-capacity Large Cooling Pan, designed to efficiently cool and solidify molten metals in various industrial applications. The pan offers a spacious and durable solution for effectively reducing the temperature of hot metal, enabling safe handling and downstream processing. With its robust construction and advanced features, our pan ensures optimal cooling performance and enhances operational efficiency.

Our pan is specifically engineered to accommodate significant volumes of molten metal, providing ample space for the cooling process. It is constructed using high-quality materials that can withstand the extreme temperatures encountered during metal casting and other industrial applications. The pan’s design features smooth surfaces and reinforced edges to facilitate easy pouring and handling of the cooled metal.

Product Parameters:
The Large Cooling Pan is available in various sizes and capacities, allowing you to select the appropriate dimensions based on your specific cooling requirements. The parameters, such as length, width, and depth, can be customized to suit your operational needs, ensuring efficient and effective cooling of the molten metal.

Product Features:
Our pan incorporates several features that contribute to its functionality and versatility:
High Cooling Efficiency: The pan’s large surface area and enhanced heat dissipation properties promote rapid and efficient cooling of the molten metal, reducing the processing time and facilitating downstream operations.
Robust Construction: Constructed from durable materials, the large pan offers excellent resistance to thermal stress and mechanical impact, ensuring long-term reliability and extended service life.
Easy Handling: The pan is designed with reinforced edges and suitable lifting mechanisms, enabling safe and convenient handling during the pouring and transport of the cooled metal.
Compatibility: Our product is suitable for a wide range of metals, including aluminum, steel, copper, and other non-ferrous alloys. It can be utilized in diverse industrial applications such as foundries, metal casting, and metalworking processes.

Product Details:
Our Large Cooling Pan is meticulously designed and manufactured to meet the highest industry standards. The pan’s dimensions, materials, and structural integrity are carefully optimized to ensure effective cooling and reliable performance. It undergoes stringent quality control measures to guarantee durability and functionality in demanding industrial environments.

Product Qualification:
Our pan is manufactured using premium-grade materials and adheres to strict quality standards. It undergoes rigorous testing to ensure its performance, durability, and compliance with industry requirements. We prioritize customer satisfaction by delivering products that meet or exceed expectations.

Shipping And Service:
We provide efficient shipping services to ensure the safe and timely delivery of our pan to your designated location. The pan is securely packaged to prevent damage during transit. Additionally, our dedicated customer support team is available to assist you with any inquiries or concerns you may have, ensuring a seamless and satisfactory experience.

Filed Under: Dross Management

October 11, 2019 By Coffy Leave a Comment

Sow Moulds and DCU (Dross Compression Unit)

DCU Dross Compression Unit — Aluminum Dross Press in Operation

DCU Dross Compression Unit for Aluminum Dross Press
DCU (Dross Compression Unit)

DCU — Dross Compression Unit for Aluminum Dross Recovery

A DCU (Dross Compression Unit) is an aluminum industry term for what is more commonly referred to as an aluminum dross press — a hydraulic compression system designed to recover free metal from hot aluminum dross at the point of generation. The terminology differs across markets and operations; the engineering objective is the same: compress hot dross rapidly under controlled hydraulic force, arrest oxidation through integrated cooling, and produce a dense aluminum block with the maximum recoverable metal content.

SMI designs, manufactures and supplies DCU systems as part of its complete aluminum dross press equipment range. SMI DCU systems are the product of over 30 years of casthouse operational experience and continuous engineering development — incorporating design improvements that directly address the geometric and thermal limitations of earlier dross compression unit designs in the industry.

Early dross compression unit designs relied on pan geometries that prioritised volume over seal integrity — a trade-off that limited recovery performance under sustained operational pressure. SMI’s DCU development addressed these geometric limitations directly: tighter mating tolerances between press head and dross pan, improved thermal seal design, and material formulations engineered specifically for the thermiting conditions of hot dross service. The result is measurably better metal recovery and longer component service life under continuous casthouse operation.


SMI Dross Compression Unit — In Operation

The following video demonstrates an SMI DCU installation in active casthouse service. This footage shows an early production configuration — current SMI DCU systems incorporate significant design and material improvements over the configuration shown, reflecting ongoing engineering development based on operational feedback from casthouse installations worldwide.

The video illustrates the core DCU operating cycle: dross pan positioning, hydraulic head descent, compression under controlled pressure, forced cooling activation, and head retraction. The automated cycle requires no manual intervention during pressing, reducing operator exposure to radiant heat and fume while eliminating the skill variability associated with manual dross handling.


DCU System Design — Key Engineering Principles

Press Head and Dross Pan — The Matched Set

The performance of any DCU system is determined primarily by the quality of the match between the press head (cooling head) and the dross pan. The two components must be designed together — the press head profile must seat correctly against the dross pan walls to maintain an effective thermal seal under hydraulic pressure and transfer heat efficiently through the cooling circuit. SMI designs and supplies press heads and dross pans as matched sets for this reason.

Proprietary Material Formulation

SMI press heads and dross pans are manufactured from a proprietary material formulation developed in-house — engineered for thermal shock resistance and dimensional stability under repeated high-temperature cycling. This formulation is the same specification used across SMI’s full range of casthouse consumables, with a 30-year operational record in aluminum casthouses across multiple continents.

Compatibility Across All Dross Types

SMI DCU systems are configured and validated for the full range of industrially relevant dross types — dry, wet, black, white, salt and rotary furnace slag. Each dross type behaves differently under compression; SMI application engineers confirm the correct press head geometry, cooling configuration and dross pan specification for each installation’s specific dross characteristics before order placement.

Upgrade and Retrofit

For operations with existing DCU or dross press installations from any manufacturer, SMI provides upgrade and retrofit supply — replacement press heads, dross pan sets and system improvements — without requiring full system replacement. Where the press frame is serviceable, targeted component upgrades can deliver significant improvements in recovery performance. All third-party press frame adaptations are subject to engineering review before supply confirmation.


Sow Moulds — Overview

SMI also supplies alloy steel sow moulds for aluminum casthouses. Sow moulds are reusable cast steel moulds used to form aluminium ingots and cast molten metal from furnaces and transfer launders. SMI sow moulds are manufactured from proprietary alloy steel formulations engineered for thermal shock resistance and long service life in continuous casthouse operation.

Standard and low-profile designs are available in multiple sizes, with options for air-cooled applications, sow feet, lugs and hooks, fork channels, and application-specific material chemistries. Custom configurations — including logo casting and dimensional modifications — are available on request. For the full sow mould product range and specifications, see the SMI Alloy Steel Sow Mould and Dross Skim Pans and Sow Moulds pages.


Related Products — Complete Dross Management from SMI

  • Aluminum Dross Press Systems — SMI40, SMI60, SMI80 and custom configurations
  • Dross Press Cooling Head — cooled and uncooled variants, all geometries
  • Dross Press Equipment Overview — system configurations and upgrade options
  • Dross Skim Pans and Sow Moulds — matched pan-and-head sets
  • Aluminum Dross Cooling Pan — rapid salt cake cooling post-press
  • Aluminum Dross Recycling Systems — full downstream processing line
  • Alloy Steel Sow Moulds
  • Ingot Molds, Sow Moulds and Dross Pans for Aluminum Scrap Recycling

Request a Quotation or Technical Consultation

To discuss DCU system requirements, press head and dross pan configuration, or sow mould specifications, please contact SMI’s application engineering team with the following information:

  • Operation type: primary smelter / secondary smelter / recycling plant
  • Furnace type and dross generation rate
  • Dross type: dry / wet / black / white / salt / rotary furnace slag
  • Existing equipment: press frame, pan set, cooling system if applicable
  • Sow mould requirements: standard / low-profile / custom dimensions

Contact SMI — DCU and Sow Mould Enquiry →

Filed Under: Dross Management Tagged With: aluminium casting, DCU, dross compression unit, Dross Press, Sow Mold

December 24, 2018 By Coffy Leave a Comment

SMI Dross Processing in Aluminum Recycling Operations

Dross Processing in Aluminium Recycling Operations — Pan Design, Press Configuration and Why Results Vary

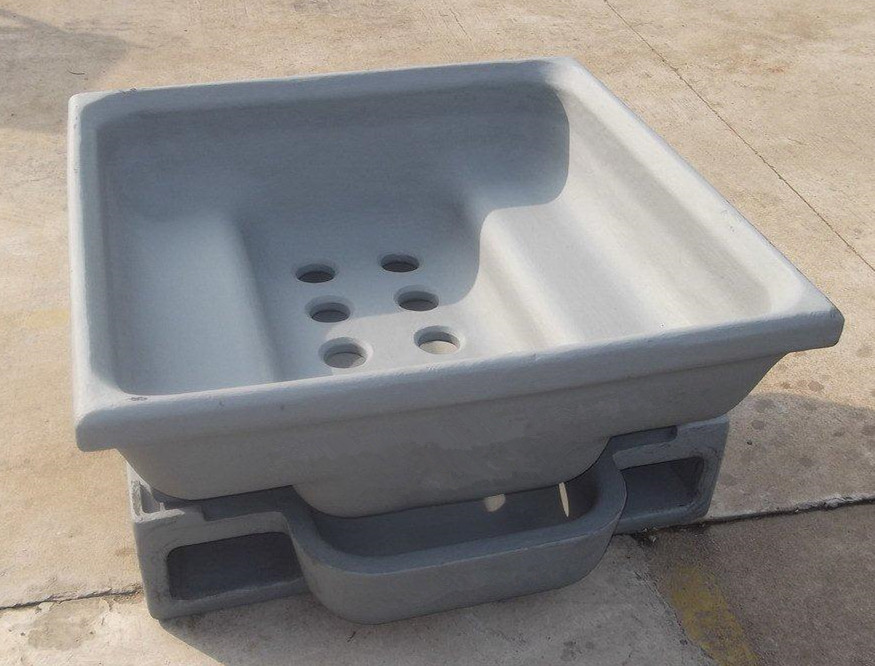
SMI alloy steel dross pan with multi-hole drain configuration and fork channels for aluminium casthouse dross processing
SMI alloy steel dross pan — multi-hole drain configuration with double counter-sink design, fork channels and large pan mass for maximum thermal cooling contact. Manufactured from proprietary alloy steel formulation for thermal shock resistance and long service life in continuous casthouse operation.

SMI has been supplying dross pans and dross press systems to the aluminium industry for over 30 years. Since 2009, Mr. David Roth has been our head consultant, bringing decades of experience in the global aluminium industry to SMI’s equipment design and customer application work.

All of the major players in aluminium melting and casting have purchased SMI quality castings. The observations in this article are drawn from that operational experience — from installations that worked well and from installations that did not, and from understanding precisely why the difference occurred.


The Dross Pan — Where Recovery Begins

The dross pan is not a passive container. Its design directly determines how much metal is recovered in the pressing cycle that follows. The unique characteristics of SMI’s dross pan design allow for a significant degree of cooling contact between the dross and the cast steel — a function of pan mass, geometry and surface area that cannot be replicated by a simple fabricated vessel.

The drain hole configuration is a specific engineering decision, not a standard feature. The number of holes and the double counter-sink design allows for the maximum drain possible without dross sticking in the holes — a failure mode that renders the drain function ineffective and forces operators to intervene manually. The distance between the skim position and the sow mould is also considered carefully in the pan design, to allow large drain volumes without the pans freezing together during the transfer process.

The cooling cycle for correctly specified dross pans is approximately two hours before the material can be rotated out. The large pan mass is critical to achieving this result — it is what drives the thermal extraction that makes the subsequent pressing cycle effective.

Some earlier pan designs in the industry relied on single-hole drain configurations. A single drain point is inherently prone to blockage given the viscosity and oxide content of hot dross — when it blocks, the entire drain function is lost. The single-chamber pan geometry also limits the cooling and plating action achievable during pressing. SMI’s multi-hole, double counter-sink design addresses both failure modes directly.

Hot aluminium dross being skimmed from furnace into SMI dross pan — casthouse operation
Hot aluminium dross being skimmed from the furnace into the dross pan — time from skimming to pressing is the critical variable in metal recovery
Liquid aluminium visible in freshly skimmed hot dross — immediate pressing required to prevent oxidation loss
Liquid aluminium visible in freshly skimmed hot dross — oxidation begins immediately after skimming
Forklift transfer of loaded SMI dross pan to aluminium dross press — fork channel design accommodates standard casthouse material handling
Forklift transfer of loaded dross pan to the dross press — pan design accommodates standard fork truck specifications for each installation

Press Capacity — The Operational Variable Most Often Underestimated

The most consistent cause of dross press underperformance in the field is not equipment quality — it is insufficient press capacity relative to the dross generation rate of the operation.

The mechanism is straightforward. Hot dross skimmed from the furnace begins oxidising immediately. The cooling and plating action that is the primary benefit of pressing — the conversion of liquid aluminium droplets into a recoverable solid block — requires the dross to reach the press while still at temperature. If a dross pan sits for more than 15 minutes before pressing, this process is already significantly compromised. The dross has cooled, the liquid aluminium has partially oxidised, and the pressing cycle produces a result that does not reflect the capability of the equipment.

When multiple pans queue in front of a single press, the pans at the back of the queue are already cold before they are processed. Operators observe poor results, conclude that pressing is ineffective, and gradually stop using the equipment — not because the press is at fault, but because the system was never configured with adequate capacity for the volume of dross being generated.

The practical implication for system specification is direct: the number of presses required for an operation is determined by the dross generation rate and the 15-minute processing window — not by capital budget alone. An undercapacity installation does not produce partial results; it produces results that appear to confirm that pressing does not work, which is a different and more damaging outcome.


The Pan and Press Head as a Matched System

The most important engineering decision in a dross press installation is the casting design of the pan and the press head as a matched pair. The press head must seat correctly against the pan walls to maintain an effective seal under hydraulic pressure — a poor geometric match allows dross to escape under compression and breaks the thermal contact that drives cooling performance.

SMI designs the pan and press head together, specifically for each customer’s furnace configuration, dross volumes and material handling capabilities — fork truck specifications, transfer distances and pan positioning. The combination of pan design and press head geometry determines the fastest possible cooling rate, the highest achievable drain volume and the most effective plating action for the specific dross type being processed.

The press itself — hydraulics, frame, automation — is in SMI’s view a delivery mechanism for the casting design. A high-quality press delivering poor results is almost always a pan-and-head geometry problem, not a press problem. SMI’s focus is on providing a high-quality, simple, low-maintenance press that fully utilises the recovery capability built into the casting design.


Operational Recommendations

Based on over 30 years of dross press installations across primary smelters, secondary smelters and recycling operations, SMI’s application engineering team consistently observes the following in operations that achieve the best results:

  • Minimise time from skimming to pressing — the 15-minute window is a real operational constraint, not a guideline. Workflow design should prioritise getting hot dross to the press as the first priority after skimming.
  • Size press capacity to dross generation rate — calculate the number of pans generated per shift and confirm that press capacity can process them all within the 15-minute window. If the numbers do not support a single press, two presses is the correct specification.
  • Specify pan and press head as a matched set — do not select the press and the pan independently. The geometric relationship between them is the primary determinant of recovery performance.
  • Maintain the pan-to-head seal — a worn or damaged mating face on either the pan or the head degrades recovery performance continuously. Replacement scheduling should be based on dimensional inspection, not visible failure.
  • Account for dross type — different furnace types and alloy practices produce dross with different characteristics. Pan and head geometry should be confirmed for the specific dross type being processed, not selected from a generic catalogue.

SMI Dross Pan Design — Key Features

Design Feature Function Failure Mode Addressed
Multi-hole drain configuration Maximum drain volume during pressing Single-hole blockage — loss of drain function
Double counter-sink hole design Prevents dross sticking in drain holes Hole blockage requiring manual intervention
Large pan mass Thermal mass drives cooling contact with dross Insufficient cooling — poor plating action
Pan-to-head matched geometry Effective seal under hydraulic pressure Dross escape and thermal seal failure under compression
Furnace-specific dimensioning Correct volume for furnace dross output Undersized or oversized pans relative to dross generation
Fork truck compatibility Safe transfer from furnace to press Handling delays that extend the pre-press window beyond 15 minutes

Related Products

  • Dross Skim Pans and Sow Moulds — matched pan-and-head sets, proprietary alloy steel
  • Dross Press Cooling Head — cooled and uncooled variants, all geometries
  • Aluminum Dross Press — SMI40, SMI60, SMI80 and custom configurations
  • Dross Press Equipment Overview — system configurations and upgrade options
  • Press Head and Dross Pan — matched configuration guide
  • Aluminum Dross Cooling Pan — post-press salt cake and dross cooling unit
  • Aluminum Dross Recycling Systems — complete downstream processing line

Contact SMI — Dross Processing Application Enquiry

To discuss dross pan and press head specification for your operation, or to review an existing installation that is not achieving expected recovery results, please contact SMI’s application engineering team. Please provide your furnace type, dross generation rate per shift, current pan and press configuration, and dross type.

SMI will respond with a written assessment and recommendation. Contact SMI →

Filed Under: Dross Management Tagged With: Aluminum Recycling, dross pan, Dross Press, dross processing, secondary smelter, SMI

  • « Go to Previous Page
  • Page 1
  • Page 2
  • Page 3
  • Go to Next Page »

Primary Sidebar

  • Home
  • About Us
  • Industries Served
    • SMI Products Overview
      • SMI Special Steel Products 01
      • SMI Special Steel Products 02
      • SMI Metal Recycling
      • NDT (Non Destructive Testing) service
  • Capabilities
    • Aluminum Industry
      • Aluminum Dross Press
      • Aluminum Dross Cooling Pan
      • Alloy Steel Sow Mold
      • Aluminum Dross Skim Blades and Skim Tools
      • Aluminum Furnace Skimming Tool or Skim blades used for Stirring and Mixing
      • Dross Press & Dross Processing
      • Application of Intelligent Ladle Slag Scraper (Skimming Tools) in steel mills and aluminum mills
      • Transmission Parts
      • The correct combination of the press head and the dross pan
      • 7-9kgs Small Standard Ingot Molds | Moldes de lingotes estándar pequeños de 7-9kgs
      • Comparison between Sow Molds and Ingot Molds
      • Aluminum Dross Transport Equipment
      • Aluminum Dross Recycling Systems
      • Aluminum, Magnesium, Brass, Bronze, Lead, Zinc Ingot Molds
      • Anode steel claw (Electrolytic claw) | Garra de acero del ánodo (garra electrolítica)
      • Anode Steel Yoke
  • eNews
  • Contact Us

Footer

Customized Products & Services

Professional Aluminum & Magnesium plant equipment supplier from China.
Up to 4,000 metric tons of mechanical products annually.
More than 30 years’ manufacturing and export experience.
Serving Global Aluminum & Magnesium smelters and metal recycling industry since 1996.

Recent Products & Services

  • High-Performance Aluminum Ingot Molds: The Complete Selection Guide
  • Casting vs Forging vs Machining: Choosing by Wear Mechanism
  • Ingot Mold Failure Modes: Causes, Prevention & Lifespan Tips
  • Global OEM Supply Chain: Heavy-Duty Crusher Wear Parts Manufacturing
  • Dross Pan Cover: Oxygen Barrier, Not Insulation

Found favorite parts & services

Sino Machine Industries — Heavy Industry Supplier with 30 Years of Manufacturing Expertise in Aluminium, Crushing & Transmission Parts. Serving primary smelters, recycling plants and OEM clients across 30+ countries. Get a free quote: [Inquiry@sinomachine.org]
  • Home
  • Privacy Policy
  • Terms of Use
  • Download Center
  • Site Map
  • Contact Us

Copyright © 2026 Sino Machine Industries (SMI) Serving Global Machinery Markets Since 1996